Object Recognition in Material Flow
Artificial intelligence based on IoT data and sensor technology for object recognition in industrial environments. Using image processing, laser technology, or AI-based algorithms, IoT solutions at other operations in our network identify moving objects based on shape, size, or coding. This enables sorting, quality assurance, or rejection to be automated directly. → These proven IIoT applications reduce error rates and accelerate processes.
Assets where this use case was implemented
Machines, devices and plants from the solution examples. The number shows how often.
How have other companies implemented this use case?
Discover solution examples from our network

Central availability of inventory data with ERP integration
Jan 30, 2023Read more →

Sharp robot gaze reduces picking error rate
Oct 15, 2021Read more →
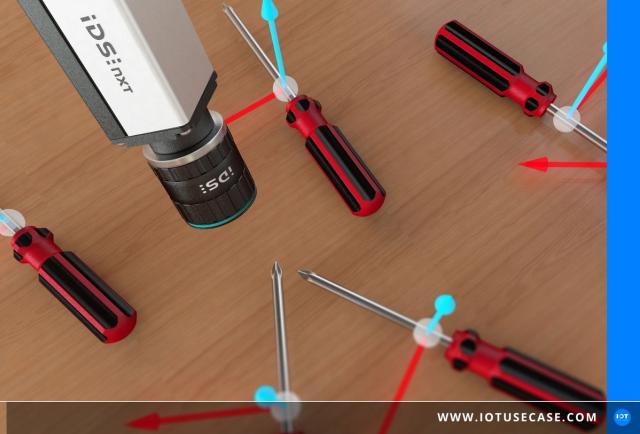
Trained pick-and-place robot with camera eyes reduces complaint and energy costs
Aug 5, 2021Read more →

Optical quality inspection with artificial intelligence
Nov 14, 2020Read more →
This use case has already been implemented. We know the people behind it.
Just ask us. We look up how your use case has already been implemented and put you in touch personally.
IoT Building Blocks


Have a concrete IoT project in mind?
We know the vendors who've already done it.